Premium Industrial Storage Solutions
Why Partner with Our Manufacturing Expertise?
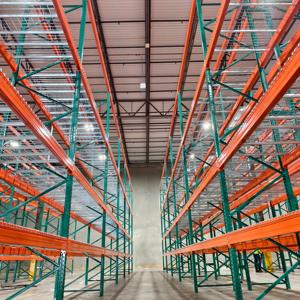
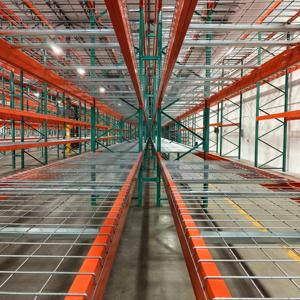
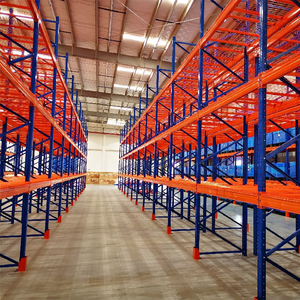
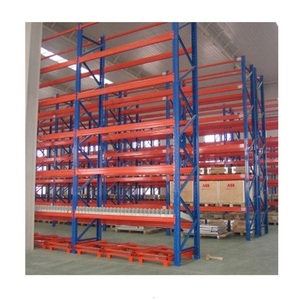
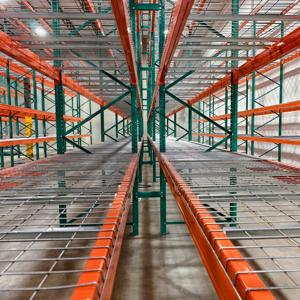
As a leading China-based industrial pallet rack manufacturer, we distinguish ourselves through rigorous adherence to international engineering standards. Our facility integrates automated roll-forming and robotic welding, ensuring that every frame and beam meets the highest seismic and load-bearing requirements. By maintaining in-house quality control and providing customized design services, we ensure that your warehouse operations benefit from optimized space utilization and peak inventory safety.
Future Procurement Trends in Warehouse Storage
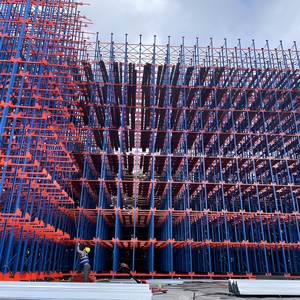
The global shift towards e-commerce and rapid logistics is driving a transformation in pallet racking. Today's procurement trends favor "Intelligence-Ready" infrastructure. Clients are increasingly asking for racking that is compatible with Automated Storage and Retrieval Systems (AS/RS), Mobile Racking systems, and pallet shuttle technologies. Sustainable design is no longer optional—modern buyers prioritize carbon-efficient manufacturing processes and long-lifecycle steel products that can withstand harsh environments, including specialized cold-storage operations.
Common Frequently Asked Questions (FAQ)
Q: How do I select the right pallet rack for my warehouse?
A: Consider your SKU density, forklift type, and local seismic codes. We provide customized layouts to balance accessibility and density.
Q: What is the lead time for export orders?
A: As a direct manufacturer, we optimize production schedules for fast shipping across North America and global markets.
Q: Do your racks meet safety standards?
A: Yes, our products are engineered according to RMI, CE, and ISO certifications to ensure global compliance and safety.